I have seen tube sheets fail in ways the material datasheet never predicted. A 316 sheet pitted through in a service that looked benign on paper, because the cooling water carried trace chlorides nobody checked. A carbon steel sheet with a perfectly good coating failed at the tube-to-tubesheet joint, because the coating never reached the crevice. Material selection gets a lot of attention in the specification, and it deserves it, but the material alone rarely decides the outcome. What decides it is whether the material suits the actual environment, and whether the fabrication detail lets the material do its job.
What the Tube Sheet Is Actually Being Asked to Do
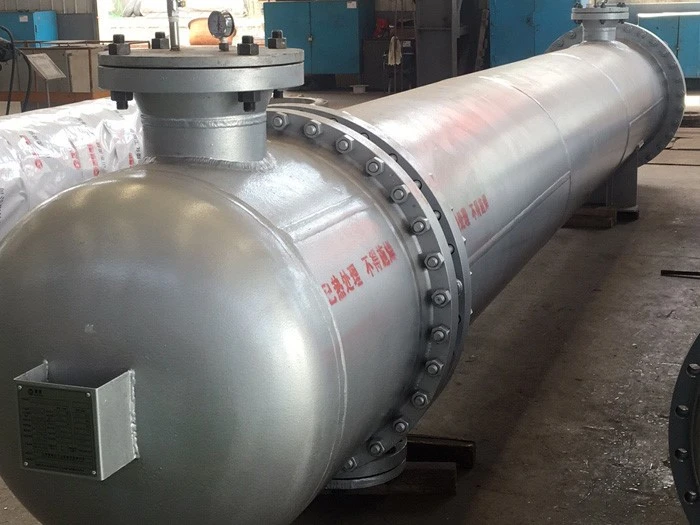
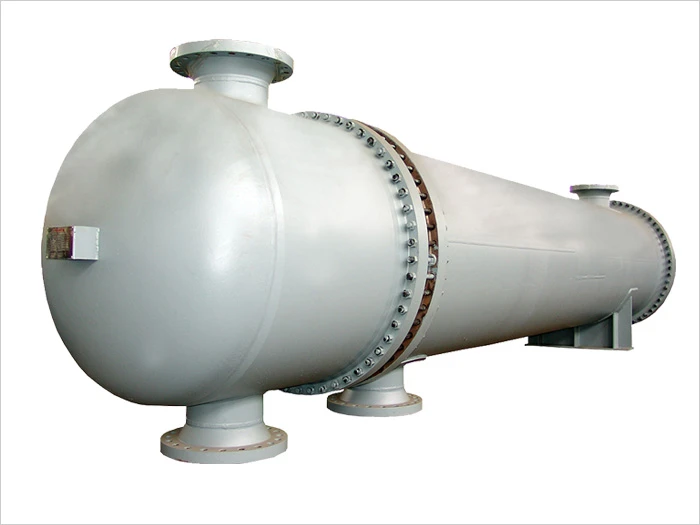
The tube sheet is a plate that separates two fluids, supports the tubes, and carries the pressure load from both sides. It is also the component where the exchanger concentrates its risk: both fluids, the pressure boundary, the crevices, and the deposits all meet on one plate.
That means the material has to do three things at once. It has to resist corrosion from both fluids. It has to have enough strength to carry the pressure and the thermal load. And it has to be fabricable, so that the tube holes, the tube-to-tubesheet joints, and the cladding can be made reliably.
Most material failures I have seen were not caused by the alloy being wrong in general. They were caused by the alloy being wrong for one specific condition, usually a trace component or a stagnant zone, that nobody assessed.
The Materials, Stated Plainly
- Carbon steel is strong and cheap. It is used for water, fuel, and many moderate services, and it relies on a coating, a lining, or a corrosion allowance. It is the right choice when the service is benign and the budget matters. It is the wrong choice when the fluid is aggressive, because a coating defect becomes a corrosion cell, and the tube-to-tubesheet crevice is the hardest place to coat.
- Stainless steel, 304 and 316, is the workhorse for chemical service, food processing, and moderate chloride environments. 316 adds molybdenum and handles chlorides better than 304. Both rely on a passive oxide layer, and both lose that layer in chlorides, in stagnant low-oxygen conditions, and in reducing acids. A 316 sheet in a chloride-rich cooling water service can pit just as badly as carbon steel, only more slowly and less predictably.
- Duplex and super duplex give higher strength and better chloride resistance than 316. They are used in seawater, offshore, and chloride-rich process service. The trade-off is weldability, and the fabrication procedure has to be qualified.
- Copper alloys have excellent thermal conductivity and are used in HVAC, marine, and some process service. They are vulnerable to stress corrosion and dezincification in aggressive environments, so the chemistry has to be checked carefully.
- Nickel alloys, such as Inconel and Monel, are used for the aggressive services where nothing else survives: hot concentrated acids, mixed acid service, and high-temperature corrosive streams. They are expensive, and they are usually specified only after a corrosion assessment confirms they are needed.
- Titanium is the default for seawater, desalination, and chloride-rich service. It is essentially immune to chloride pitting in most operating ranges, but it is expensive, and it has its own limits, including dry chlorine and some reducing acids.
Clad plate is the practical answer for many projects. A carbon steel sheet with a stainless, duplex, or titanium cladding gives corrosion resistance on the wetted face while the carbon steel carries the structural load. It is usually cheaper than a solid alloy plate. The cladding thickness and the bond quality are the critical details, because an unbonded area becomes a corrosion cell.
What Actually Determines Whether the Tube Sheet Lasts
The datasheet will give you the alloy and the thickness. It will not tell you the things that decide whether the tube sheet survives.
This is the first input, and it is the one most often skipped. You need the actual fluid composition on both sides, including trace chlorides, the temperature, the pH, and the oxygen level. A general chemical resistance chart is not enough. Trace chlorides from cooling water are the most common cause of stainless tube sheet failures I have seen.
The tube and the tube sheet are usually different materials, and that is where galvanic corrosion starts. The joint detail, whether expanded, welded, or both, has to be compatible with both materials and with the fluid in the crevice.
If clad plate is used, the bond has to be verified. An unbonded area is a corrosion cell and a potential failure point. Ask for the bond inspection records.
Some materials are difficult to weld or machine, and the fabrication quality affects corrosion resistance. A duplex sheet with a poor weld procedure can lose its corrosion resistance at the heat-affected zone. A titanium sheet requires inert gas shielding, and a poor weld is a corrosion site.
Deposits settle where the flow is slow, and that is where pitting starts. The baffle design and the nozzle detail matter as much as the alloy.
Most tube sheet problems I have seen were fabrication or operation problems, not material problems.
The tube holes have to be clean and burr-free before the tubes are inserted. The expansion or welding has to follow the qualified procedure. The tube sheet face has to be protected during handling and assembly. The gaskets have to be the correct material and the correct thickness, and they should be replaced every time the joint is opened.
Once in service, the routine matters more than the hardware. Monitor the tube-side and shell-side pressure drop and the temperature approach. A change in either is usually the first sign of a leak or a fouling problem. Inspect the tube sheet face, the tube-to-tubesheet joints, and the area under the pass partition on a defined interval, especially in chloride service. Clean the face and the tube ends during every shutdown. If the tube sheet is clad, inspect the cladding for damage at every shutdown, because a cladding breach is a corrosion cell waiting to happen.